
Mapa mental
production
Contenido del mapa
production
casting
- tupes of casting
- liquid-> casting
- viscous->plastic processe
- powder-> metalurgy (sintering)
- advantages
- complex shapes
- large products one piece
- mostly cheap
- isotropic final product
- side notes
- draft angles
- hot material= bigger volume
- alu-> 6.6 % an al ruler of 1 mm
- LxBxH - 6,6 % = 1 meter
- 1 mm on the ruler is 1,026 mm in real
- LxBxH - 6,6 % = 1 meter
- alu-> 6.6 % an al ruler of 1 mm
- types of molds
- expendable
- sand
- no size limit
- low tooling cost
- course surface
- mostly for metals
- ceramic
- high accuracy
- high production rate
- (shell moulding)
- sand
- permanent ( metal molds)
- metal molds
- good finsish
- high accuracy
- limited complexicity
- high mould cost
- automatic
- composit
- both expendable and permanent
- expendable
- tupes of casting
shaping and forming
- continueus processes
- rolling
- flat
- shape
- metal rolling
- max thickness depends on the friction coeficient
- smaller diameters of rolls is better surface finish
- extrusion
- moderate to high equipment cost
- high temp-> low ductillity
- low temp-> high ductillity
- pulled extrusion (wire)
- always cold ( annealed first)
- even deformation
- anisotropic
- hardens, so the thin part is as strong as the thick part
- pipe is drawn with a floating mandril
- rolling
- discrete processes
- forging
- hot forging
- lower forces
- worse surface finish
- anisotropic behavour
- cold forging
- good surface finish
- high forces
- crystal deformation
- high stresses
- hot forging
- forging
- continueus processes
separating processes
- separating: removing material without changing structure hardly any material is lost
- mechanical
- with chips
- sawing
- grinding
- wet
- upto 50m/s
- dry
- up to 100m/s
- more expensive than milling
- very accurate
- good for hard materials
- grinding ratio:
- G= dVworkpiece/dVdisc
- wet
- milling
- climb milling
- clamps material down
- conventional milling
- better for hard top layer
- pack mill
- can drill
- not symetrical
- end mill
- can not drill
- comes in from the side
- climb milling
- broaching
- without chips
- cutting
- punching
- punching
- force liniar with
- perimeter
- shear strength
- sheet thickness
- punch inside outwards
- diameter of punch should be less than the sheet thickness
- force liniar with
- blanking
- parting
- shear angle of the punch aprx 12 deg
- punching
- with chips
- physical
- flame
- plasma
- high speed
- strong ionisation of gass
- smooth
- laser
- high temp
- narrow cut
- small heat affected zone
- hampered by reflection and construction
- problem: cuts through everything
- laser drilling
- very accurate
- laser bending
- bending with heat
- badly controlled proces
- independent of mechanical properties
- based on concentrated energy
- narrow cut
- heat affected zone (bleu oxide)
- wire edm
- electrode wire dia 0,05 to 0,5 mm
- speed up to 2,5 mm/sec
- dieelectric fluid is not conductive
- alternating current
- gap with of 5-> 100 micrometer
- electrical discharge machining
- machining
- tool charastaristics
- toughness
- thermal shock resistance
- wear resistance
- chemical stabillity and inertness
- ISO classifications
- example: HC-p 15
- HC=coated
- p= workpiece material
- 15= mechanical load
- example: HC-p 15
- cutting speed
- tool steel
- Vc<0,2 m/s
- high speed steel
- Vc 0,3 to 0,5 m/s
- hard metal
- Vc 1,5 to 3 m/s
- coated carbide
- Vc 6 m/s
- ceramic
- Vc 20 m/s
- cubic boron nitride
- Vc 5m/s
- diamond
- tool steel
- tool life
- Vc * T ^n = C
- Vc = cutting speed
- T = tool life
- ^n = constand
- c = constant
- Vc * T ^n = C
- tool charastaristics
- ecm
- electrical chemical machining
- conductive fluid
- fast
- 5-20 Volt
- 10.000 Amp
- no toolwear
- non alternating current
- (electro etching)
- conductive electrode
- chemical machining
- chemical attack
- no current
- (acid etch)
plastics
- plastic= polymer with additive
- fillers:
- sawdust
- chalk
- plasticisers
- soft and flexible
- anti scission
- protect for UV radiation
- protect against oxigen
- collorant
- organic dye
- flame retardent
- chlorine
- bromine
- phosphorus
- lubricants
- reduce friction during production
- reduce sticking during production
- fillers:
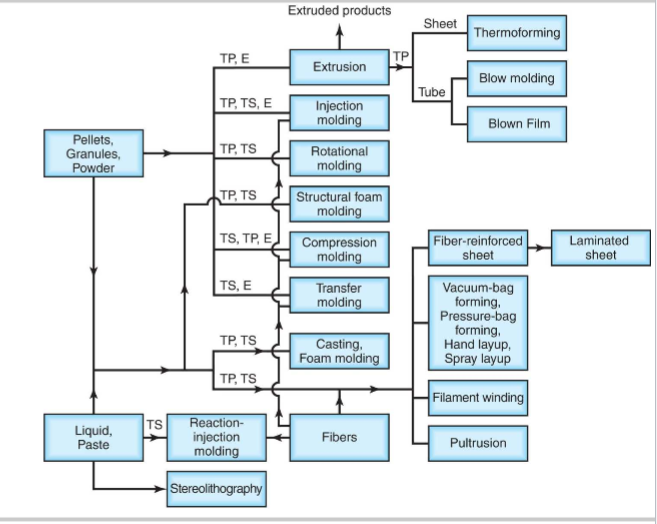
- types of plastic
- TP
- thermoplast
- TS
- thermosetting
- E
- elastomer
- TP
- extrusion blowmoulding
- injection blowmoulding
- rotational moulding
- plastic= polymer with additive
new processes
- additive manufacturing
- stereo lithiografie
- printing with light beam in fluid
- fast start of production
- process gradually builds the prioduct
- low production speed
- small batches
- complex shapes
- no advantages of scale production
- speeds up the design process -> prototyping
- can be custom made
- low amount of waste
- weight reduction
- only strength were required
- topological optimisation
- fused deposit manufacturing(3d printing)
- laser sintering
- 3d printing with gleu in chalk
- stereo lithiografie
- additive manufacturing
Imágenes y archivos del mapa
Información
- Descripción
- Mapa Mental sobre production, creado por Martijn de vos el 19/01/2019.
- Creado por
- Martijn de vos
- Visitas
- 0
- Historial
-
- Creado por Martijn de vos · 19 ene 2019
- Copiado por Martijn de vos · 19 ene 2019
- Valoración